Locking Cylinder Model Group

Locking Cylinder Model Group

Locking Cylinder Model Group: Pilot-Operated Check Valves for Secure Load Holding

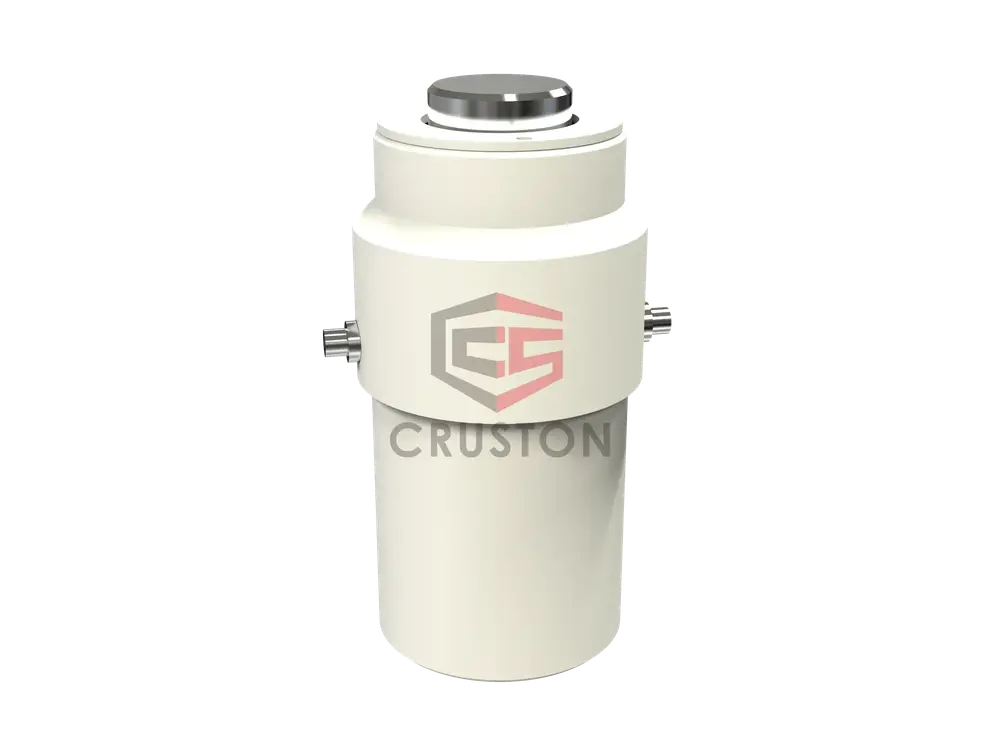
The locking cylinder model group comprises hydraulic locking cylinders with integrated pilot-operated check valves, available in bore sizes from 20 mm to 100 mm and rated pressures of 70 to 210 bar. These cylinders are designed to hold loads securely in position without pressure loss, making them suitable for applications in construction machinery, agricultural equipment, and industrial automation.

Rated Pressure
70-210 bar
Body Material
Hard chrome-plated steel
Seal Material
NBR (Buna-N)
Mounting Type
Clevis or flange

How Does the Locking Cylinder Model Group Ensure Reliable Load Holding in Hydraulic Systems?

The locking cylinder model group consists of double-acting hydraulic cylinders equipped with pilot-operated check valves that prevent unintended retraction under load. Bore diameters range from 20 mm to 100 mm, with rated pressures from 70 bar to 210 bar, covering a thrust range of approximately 2.2 kN to 165 kN at maximum pressure. The valve opens only when pilot pressure is applied, ensuring the load remains locked even if supply pressure drops. This design is critical for applications requiring precise position holding, such as aerial work platforms, forklift masts, and hydraulic presses. The cylinders are constructed with hard chrome-plated steel bodies and NBR seals, compatible with mineral oil-based hydraulic fluids.

Typical applications include construction equipment (excavator arms, loaders), agricultural machinery (tractor lifts), and industrial automation (clamping fixtures, lift tables). The locking mechanism addresses the common pain point of load drift due to internal leakage in standard cylinders, enhancing safety and energy efficiency. For instance, in a 50 mm bore cylinder at 160 bar, the locking valve prevents drift even under continuous load, reducing the need for constant pump operation. The model group offers flexibility with mounting options such as clevis or flange, and stroke lengths customizable to customer requirements.

Compared to other models in the series, the 20-100 mm bore range provides a balanced solution for medium-duty applications, bridging the gap between compact cylinders (below 20 mm) and heavy-duty cylinders (above 100 mm). The 70-210 bar pressure rating ensures compatibility with standard hydraulic power packs, while the -20°C to +80°C temperature range suits most industrial environments. The integrated locking valve eliminates the need for external circuitry, saving space and reducing installation complexity. This makes the Locking Cylinder Model Group a cost-effective choice for OEMs and MRO customers seeking reliable load holding without compromising on performance.

  • Pilot-operated check valve with cracking pressure of 2-3 bar ensures reliable locking and minimal pressure loss.
  • Hard chrome-plated piston rod with surface hardness of 50-60 HRC provides excellent wear resistance and corrosion protection.
  • NBR seals rated for -20°C to +80°C and compatible with mineral oil, extending service life in harsh conditions.
Core Technical Features and Quantified Advantages

STEP 1

Pilot-Operated Check Valve with 2-3 bar Cracking Pressure

The integrated pilot-operated check valve opens at a pilot pressure of 2-3 bar, ensuring reliable locking of the cylinder under load. This valve prevents reverse flow until pilot pressure is applied, eliminating load drift caused by internal leakage. The cracking pressure is precisely set to balance responsiveness and energy efficiency, reducing pilot pressure requirements by up to 30% compared to conventional check valves. The valve is tested for 100,000 cycles without failure, ensuring long-term reliability in demanding applications.

STEP 2

Bore Diameter Range 20-100 mm with Thrust up to 165 kN

The model group covers bore diameters from 20 mm to 100 mm, providing thrust forces from approximately 2.2 kN to 165 kN at 210 bar. This range allows selection for medium-duty applications such as lift tables, clamping systems, and mobile equipment. The cylinders are designed with a safety factor of 1.5, with proof pressure tested at 1.5 times the rated pressure. The 100 mm bore model delivers 165 kN at 210 bar, suitable for heavy loads, while the 20 mm bore model offers compact size for space-constrained installations.

STEP 3

Hard Chrome-Plated Steel Body with 50-60 HRC Surface Hardness

The cylinder body and piston rod are made of steel with a hard chrome plating that achieves a surface hardness of 50-60 HRC. This plating provides excellent wear resistance and corrosion protection, extending the cylinder's service life in harsh environments. The chrome layer thickness is 20-25 μm, tested to withstand 500 hours of salt spray without red rust. The body is also treated with a anti-corrosion primer, ensuring durability in outdoor and humid conditions.

STEP 4

NBR Seals for -20°C to +80°C and 500,000 Cycles

NBR (Buna-N) seals are used throughout the cylinder, rated for operating temperatures from -20°C to +80°C. These seals are compatible with mineral oil-based hydraulic fluids and offer excellent resistance to wear and compression set. The seal design includes a double-lip wiper to prevent contamination ingress, and the piston seal is tested for 500,000 cycles without leakage. This ensures reliable performance in applications with frequent cycling, such as automated production lines and mobile machinery.

FAQs about Locking Cylinder Model Group

Similar Models