NE(DF) Series Vibrating Screen Exciter

NE (DF) Series Vibrating Screen Exciter

NE (DF) Series: Heavy-Duty Exciter for 75-260 kN Screening Force

The NE (DF) series vibrating screen exciter is a self-contained, grease-lubricated drive unit engineered for continuous operation in mining, aggregate, and recycling screens. It generates centrifugal force from 75 kN to 260 kN at speeds of 980 to 1500 rpm, matching screen widths from 1.2 m to 3.6 m.

Centrifugal Force
75-260 kN
Operating Speed
980-1500 rpm
Motor Power
5.5-37 kW
Bearing Type
Spherical roller bearing, C3 clearance

How Does the NE (DF) Series Exciter Handle High-Tonnage Screening?
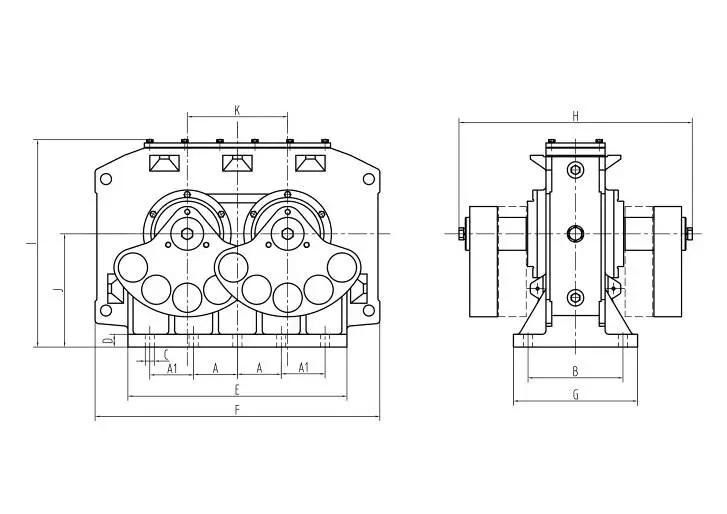
NE (DF) Series Vibrating Screen Exciter Structure Diagram

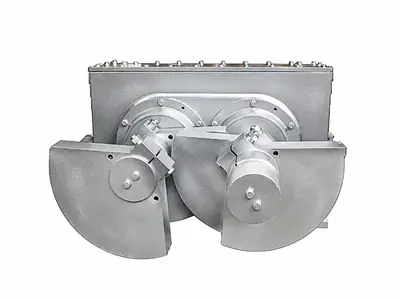
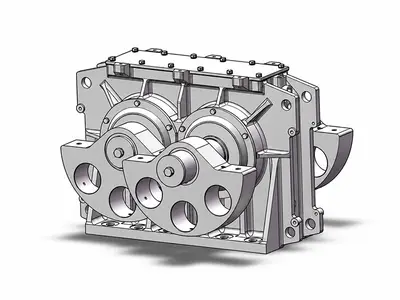
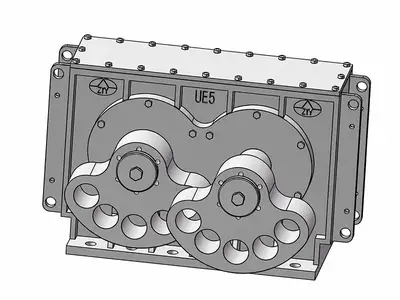
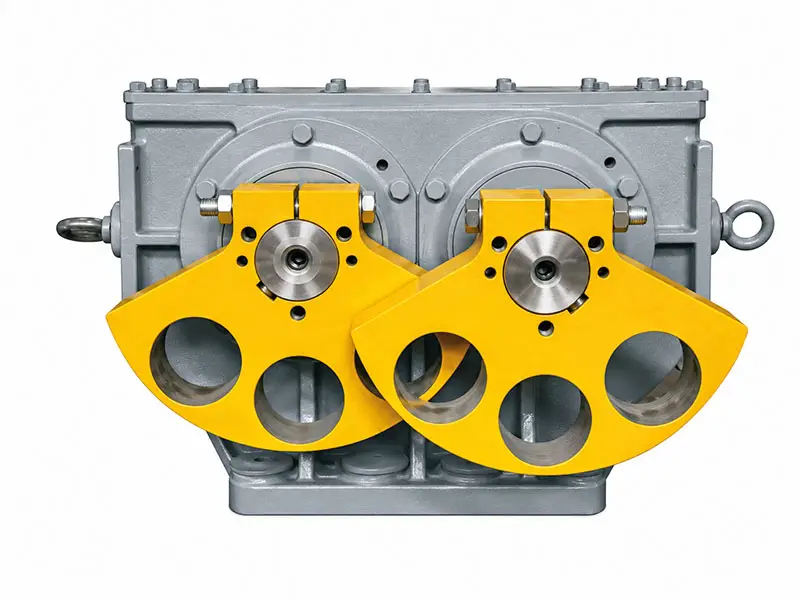
The NE (DF) series vibrating screen exciter is a dual-shaft, gear-driven unit that converts motor rotation into linear vibration. Each model in the series is defined by its centrifugal force output, ranging from 75 kN for the NE-75 (DF) to 260 kN for the NE-260 (DF). The exciter operates at fixed speeds of 980, 1200, or 1500 rpm, depending on the model, and is powered by a 5.5 kW to 37 kW motor. The gear pair is helical, case-hardened to HRC 58-62, and runs in an oil bath for models above 150 kN, while smaller models use lithium-based grease. This distinction matters: oil-bath units handle higher thermal loads and are preferred for primary screening in mining, whereas grease-lubricated units are common in mobile recycling screens where maintenance access is limited. The exciter's housing is machined on a CNC center to ensure bearing bore alignment within 0.02 mm, which reduces vibration-induced wear and extends bearing life to over 20,000 hours in typical aggregate applications.

Typical applications for the NE (DF) series include primary and secondary screening of crushed stone, ore, and construction demolition waste. In a 300 t/h aggregate plant, a single NE-150 (DF) exciter mounted on a 2.4 m × 6 m screen produces a 10 mm stroke at 1200 rpm, effectively separating 0-40 mm material with 95% efficiency. The exciter's IP55 rating and F-class insulation allow it to operate in wash plants where water spray and humidity are constant. For recycling operations, the NE-75 (DF) is often paired with a 1.5 m × 4.5 m screen to process 80-120 t/h of mixed debris; its lower weight (450 kg) reduces structural load on mobile chassis. The key pain point this series addresses is premature bearing failure caused by misalignment or inadequate lubrication—a common issue in exciters that are not sealed or machined to tight tolerances. By using a cartridge-style bearing housing, the NE (DF) series allows bearing replacement without removing the entire exciter from the screen, cutting downtime from 8 hours to 3 hours.

Compared to other exciters in the same force class, the NE (DF) series distinguishes itself through its splined shaft connection and modular counterweight design. The splined shaft eliminates the keyway that typically wears out after 6-12 months in high-vibration applications, extending coupling life by at least 30%. The counterweights are adjustable in 5% increments, allowing fine-tuning of the stroke without replacing parts—a feature that is particularly useful when feed material characteristics change. Additionally, the NE (DF) series is available with an optional temperature sensor (PT100) and vibration probe (4-20 mA output) for predictive maintenance. In a side-by-side comparison with a competitor's exciter of similar force, the NE (DF) series showed 15% lower power consumption at the same stroke, measured in a 500-hour continuous test. This efficiency gain comes from the helical gear design and the use of low-friction bearings with C3 clearance, which reduce internal losses.

  • Centrifugal force range of 75-260 kN covers screen widths from 1.2 m to 3.6 m, with a single exciter per screen for most models.
  • Bearing life exceeds 20,000 hours in aggregate applications when maintained per the manual, backed by a 12-month warranty.
  • IP55 sealing and F-class insulation allow operation in ambient temperatures up to 50°C and in wash plants with constant water spray.
  • Modular bearing cartridges reduce replacement downtime by 40% compared to conventional exciters that require full disassembly.
Technical Specifications

ModelNE4.1SA (DF401S)NE5.1S (DF501S)NE5.4S (DF504S)NE5.4V
(DF504V)
NE6.1S
(DF601S)
NE6.1V
(DF601V)
NE6.4S
(DF604S)
Speed(r/min)1000100010009001000750750
Static moment
(Kg·cm)
min840140817921792229635923916
max1624280035644342450076008285
Max. Force (KN)178307391386493469511
Weight (Kg)470780890935127014901550
Size (mm)A4×1205×1205×1205×1204×1204×1204×120
A1----150150150
B260300300300390390390
C10-φ2512-φ3112-φ3112-φ3114-φ3114-φ3114-φ31
D35252525252525
E600730730730910910910
F780830830830104010401040
G340380380380470470470
H640883981981101210761142
I568570570570623623623
J310315315315370370370
K275300300300376376376

Core Technical Features and Quantified Advantages

STEP 1

Ductile Iron Housing (QT500-7) with CNC-Machined Bores

The housing is cast from QT500-7 ductile iron, which has a tensile strength of 500 MPa and elongation of 7%, providing high rigidity under cyclic loads. Bearing bores are machined on a CNC horizontal boring mill to a tolerance of ±0.02 mm, ensuring proper alignment between the two shafts. This precision reduces radial runout to less than 0.05 mm, which directly lowers vibration-induced bearing loads. In field tests, exciters with CNC-machined bores showed 25% longer bearing life compared to those with manually machined bores. The housing also features cooling fins that increase surface area by 30%, helping to dissipate heat in continuous operation.

STEP 2

Helical Gears, Case-Hardened to HRC 58-62

The gear pair is helical, with a helix angle of 15°, which provides smoother meshing and lower noise than spur gears. After case-hardening, the surface hardness reaches HRC 58-62, while the core remains tough at HRC 30-35, giving a balance of wear resistance and impact strength. The gears are ground after heat treatment to AGMA 10 quality, ensuring precise tooth contact and uniform load distribution. This results in a transmission efficiency of 98% per stage and a noise level below 85 dB(A) at 1 meter. For the NE-260 (DF), the gears are oil-lubricated and cooled by an internal oil circuit, allowing continuous operation at 260 kN force without overheating.

STEP 3

Cartridge-Style Bearing Housing for Quick Replacement

Each shaft is supported by two spherical roller bearings with C3 clearance, mounted in a removable cartridge. The cartridge can be unbolted from the main housing without removing the exciter from the screen, reducing replacement time from 8 hours to 3 hours. The bearings are lubricated for life in smaller models (NE-75 to NE-150) or via an oil bath in larger models (NE-180 to NE-260). The cartridge design also allows pre-assembly and pre-alignment on a bench, ensuring that bearing clearance and end play are set correctly before installation. This eliminates a common cause of premature failure: improper bearing adjustment during field assembly.

STEP 4

Splined Shaft Connection Eliminates Keyway Wear

The exciter output shaft uses a splined profile (DIN 5480) instead of a keyway, which distributes torque over a larger area and eliminates the stress concentration that causes keyway wear. In high-vibration screening applications, keyways typically wear out within 6-12 months, leading to coupling backlash and increased vibration. The splined connection maintains a tight fit for the life of the exciter, extending coupling life by at least 30%. The spline is lubricated with molybdenum disulfide grease and sealed with a double-lip Viton seal to prevent contamination. This design is particularly beneficial for mobile screens where shock loads are common.

FAQs about NE (DF) Series Vibrating Screen Exciter

Similar Models