NE (HE) Series Vibrating Screen Exciter

NE (HE) Series Vibrating Screen Exciter

NE (HE) Series Exciter: 75-260 kN Force for Heavy-Duty Screening

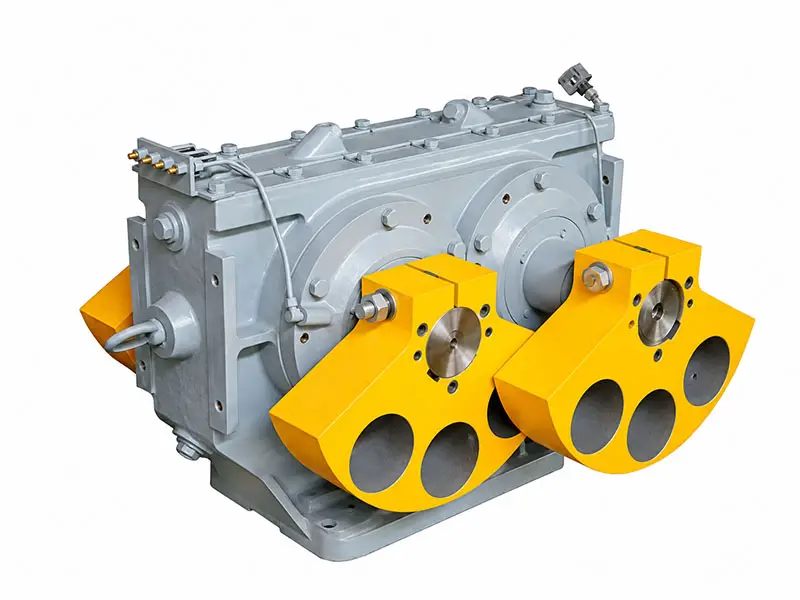
The NE (HE) series vibrating screen exciter is a self-contained, universal-joint driven vibration unit engineered for continuous operation in mining, quarrying, and coal preparation plants. Unlike motor-vibrator designs, this exciter uses a robust cast housing with precision-ground helical gears and heavy-duty spherical roller bearings to generate centrifugal forces from 75 kN to 260 kN at speeds of 980, 1200, or 1500 rpm.

Centrifugal Force
75 kN to 260 kN
Operating Speed
980 rpm, 1200 rpm, 1500 rpm
Motor Power
5.5 kW to 37 kW
Protection Grade
IP55

How Does the NE (HE) Series Exciter Improve Screening Efficiency?
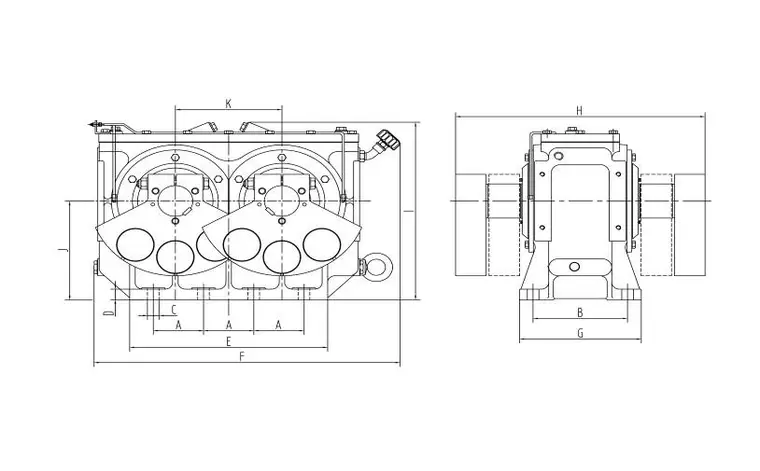
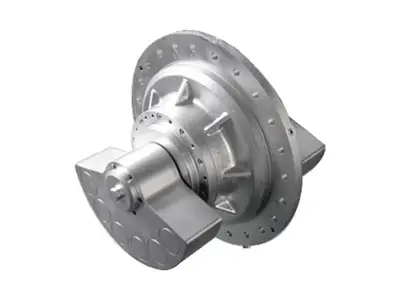
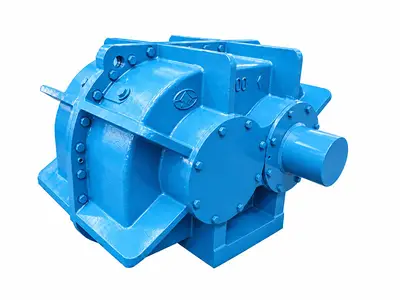
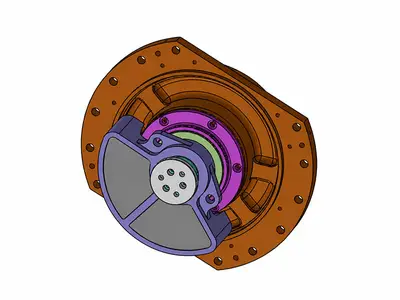
NE (HE) Series Vibrating Screen Exciter Structure Diagram

The NE (HE) series exciter is a gear-driven vibration unit that converts motor rotation into linear or circular motion for vibrating screens. Each model is defined by its maximum centrifugal force: NE-60 delivers 75 kN, NE-90 delivers 110 kN, NE-120 delivers 150 kN, NE-150 delivers 185 kN, NE-180 delivers 215 kN, NE-220 delivers 240 kN, and NE-260 delivers 260 kN. Operating speed options include 980 rpm for high-stroke applications, 1200 rpm for standard screening, and 1500 rpm for fine screening. The exciter housing is cast from high-tensile GG25 cast iron, and the gear pair is case-hardened 20CrMnTi steel with a surface hardness of HRC 58-62. This construction allows continuous operation at ambient temperatures from -20°C to +40°C without derating.

Typical applications include primary and secondary screening of crushed stone, ore, and coal. In a 300 t/h aggregate plant, two NE-150 exciters mounted on a 2.4 m × 6 m screen produce a 12 mm stroke at 980 rpm, effectively separating 0-5 mm fines from 5-20 mm aggregates. The oil-splash lubrication system requires only 2.5 liters of ISO VG 220 gear oil per exciter, with oil change intervals of 2,000 hours. This reduces maintenance downtime compared to grease-lubricated motor vibrators, which typically need re-greasing every 200 hours. The exciter's IP55 rating and F-class insulation allow operation in wash plants where water spray and humidity are constant.

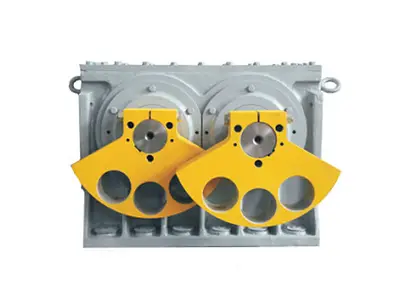
Compared to other exciters in the same force class, the NE (HE) series offers a distinct advantage in serviceability. The counterweights are externally mounted and can be adjusted without removing the exciter from the screen. A single exciter can be re-phased from 0° to 180° in 15° increments to change the motion from linear to elliptical. This flexibility means one exciter model can serve multiple screen types, reducing spare parts inventory. Additionally, the bearing housing is designed with a labyrinth seal and a grease purge port, which extends bearing life to over 20,000 hours in dusty conditions. For plants that run 24/7, this translates to fewer unplanned stoppages and lower total cost of ownership.

  • Gear-driven design with 98% mechanical efficiency, reducing energy consumption by up to 15% compared to belt-driven exciters.
  • External counterweight adjustment allows force changes in 5% increments without disassembly, cutting maintenance time by 50%.
  • Oil-splash lubrication with 2,000-hour oil change intervals and a 20,000-hour bearing life (L10h) under continuous load.
Technical Specifications

ModelNE30
(HE30)
NE65
(HE65)
NE80
(HE80)
NE100
(HE100)
NE150
(HE150)
Speed (r/min)980980980980980
Static Moment
(Kg·cm)
min5831404211628604290
max13293052437653847500
Max. Force (kN)140321461567790
Weight (Kg)410760112015301680
Size(mm)A3×1103×1403×1655×1605×160
B200250310370370
C8-φ258-φ388-φ3812-φ3812-φ38
D3045454545
E400510650980980
F87395599311331133
G270340400480480
H618780820762920
I507601663790790
J300360370465465
K250300350400400

Core Technical Features and Quantified Advantages

STEP 1

High-Tensile Cast Iron Housing (GG25)

The exciter housing is cast from GG25 gray iron with a tensile strength of 250 MPa and a Brinell hardness of 180-220 HB. This material absorbs vibration and resists deformation under the 260 kN centrifugal force of the NE-260 model. The housing wall thickness is 18 mm at the bearing seats, providing a safety factor of 2.5 against fatigue cracking. Each housing is pressure-tested at 0.5 bar for 10 minutes to ensure no porosity leaks.

STEP 2

Case-Hardened Helical Gears (20CrMnTi)

The gear pair is made from 20CrMnTi alloy steel, case-hardened to HRC 58-62 with a case depth of 1.2-1.5 mm. The helical tooth profile provides a contact ratio of 2.3, reducing noise to 85 dB(A) at 1 meter. The gears are precision-ground to AGMA Class 10, ensuring uniform load distribution and a service life of 15,000 hours. This design eliminates the risk of tooth breakage common in straight-cut gears under shock loads.

STEP 3

Spherical Roller Bearings with Labyrinth Seals

Each exciter uses two double-row spherical roller bearings (e.g., 22320 for NE-150) with a dynamic load rating of 620 kN. The bearings are lubricated by oil splash and protected by a triple-labyrinth seal with a grease purge port. This sealing arrangement keeps dust and water out, achieving an L10h life of 20,000 hours at 1200 rpm and 150 kN load. The bearings can be re-greased every 2,000 hours without removing the exciter.

STEP 4

Adjustable Counterweights in 5% Increments

The exciter's centrifugal force can be adjusted from 60% to 100% of maximum by adding or removing external counterweight plates. Each plate weighs 2.5 kg and changes the force by 5% (e.g., 7.5 kN for NE-150). This allows operators to fine-tune the stroke for different feed materials without replacing the exciter. The counterweights are secured with M20 bolts torqued to 400 Nm, and the adjustment can be done in under 30 minutes.

FAQs about NE (HE) Series Vibrating Screen Exciter

Similar Models