How Does the NE (ML) Series Exciter Improve Screening Efficiency?
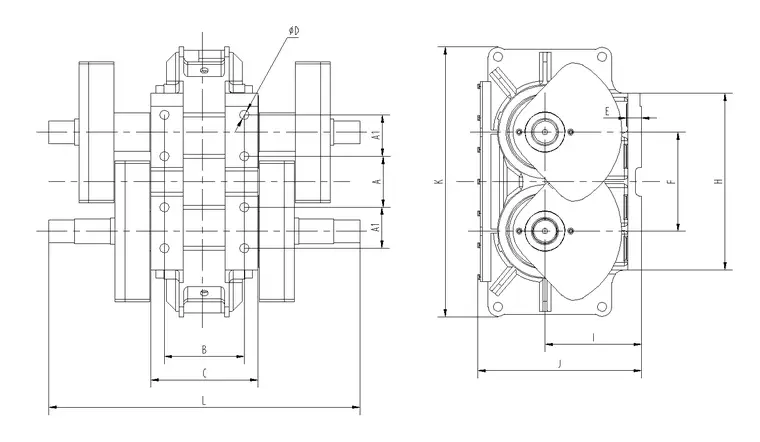
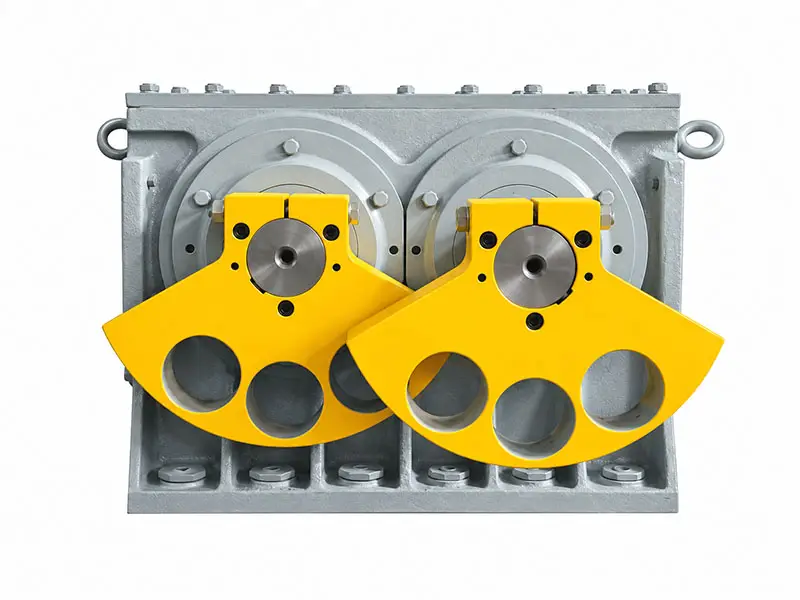
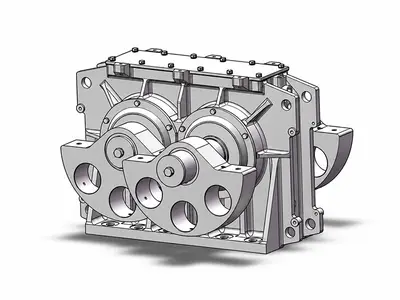
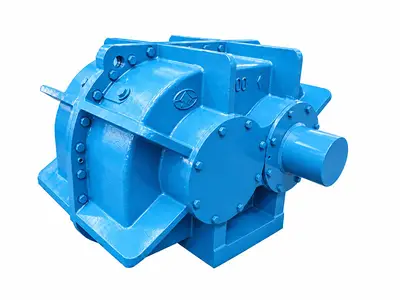
The NE (ML) series vibrating screen exciter is a critical component in high-capacity screening operations. It converts electrical motor power into a controlled vibratory force through a pair of counter-rotating shafts equipped with eccentric weights. The gearbox housing is made from high-strength cast steel (ASTM A216 WCB) and machined to tolerances of ±0.02 mm, ensuring precise gear alignment and minimal noise. The unit is available in six models, with excitation forces ranging from 50 kN to 300 kN and operating speeds from 750 to 1500 rpm. This range allows operators to match the exciter to specific screen sizes and material characteristics, from fine coal particles to large rock aggregates. The exciter is designed to withstand radial loads up to 450 kN and axial loads up to 120 kN, providing a safety factor of at least 2.5 against peak dynamic forces.
In mining and quarrying, screening efficiency directly impacts throughput and product quality. The NE (ML) series addresses common pain points such as premature bearing failure, gear wear, and oil leakage. Its spherical roller bearings (SKF or equivalent) are rated for an L10 life of 100,000 hours under normal load conditions. The gears are case-hardened and ground to AGMA 12 quality, reducing noise and vibration. The oil lubrication system uses a splash-and-circulation method, with a 12-liter oil sump that allows operation for up to 6,000 hours between oil changes. This is particularly beneficial in remote locations where maintenance access is limited. The exciter is also equipped with temperature and vibration sensors (optional) that can be connected to a plant-wide monitoring system, enabling predictive maintenance and reducing unplanned downtime.
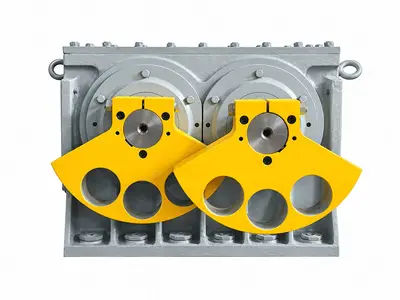
Compared to other exciters in the same class, the NE (ML) series stands out for its modular design. The eccentric weights can be adjusted without dismantling the entire unit, allowing quick changes to the excitation force. The housing is split horizontally, which simplifies inspection and replacement of internal components. Additionally, the NE (ML) series uses a unique double-labyrinth seal with grease purging, which has been proven to reduce dust ingress by up to 90% compared to standard lip seals. This is especially important in coal and cement plants where airborne dust is highly abrasive. The exciter is also available with an optional forced lubrication system for high-speed applications above 1200 rpm, ensuring adequate oil flow to all bearings and gears.
- Excitation force from 50 kN to 300 kN, with a safety factor of 2.5 against peak loads.
- Spherical roller bearings with L10 life of 100,000 hours, reducing maintenance costs.
- Double-labyrinth seal with grease purging reduces dust ingress by up to 90%.
- Modular design allows eccentric weight adjustment without full disassembly.
- Optional sensors for temperature and vibration enable predictive maintenance.